How to Choose a Precision Plastics Manufacturer?
Choosing a precision plastics manufacturer is not just a price comparison. It is a decision about process control, engineering support, and consistent part quality. A molded component may look simple on a drawing, yet a small change in wall thickness can affect filling, cooling, and warpage. The right supplier should ask detailed questions before quoting. What resin will meet the application’s needs? How will critical dimensions be measured? Can the tool produce stable parts across repeated runs?
Plastics engineering professor David Kazmer’s design-for-manufacturing guidance can be paraphrased this way: connect part design, tooling, and process control before production begins. That connection matters. Ask for examples of similar parts, documented inspection methods, and clear plans for addressing defects. A polished capability sheet helps, but actual process evidence is stronger. Details matter.
Compare suppliers on more than equipment lists. Review mold maintenance practices, material traceability, measurement tools, and communication during design changes. Ask who owns each decision, and how problems reach the people who can fix them. A short trial run can reveal issues that a presentation cannot. Still, no checklist catches everything. Supplier claims need verification, and even experienced teams can overlook a risk. A careful selection process reduces uncertainty; it does not remove it. This guide explains the questions and evidence that help identify a capable precision plastics partner for your product and production needs.
Define Resin, Geometry, and Tolerances with ISO 20457:2018
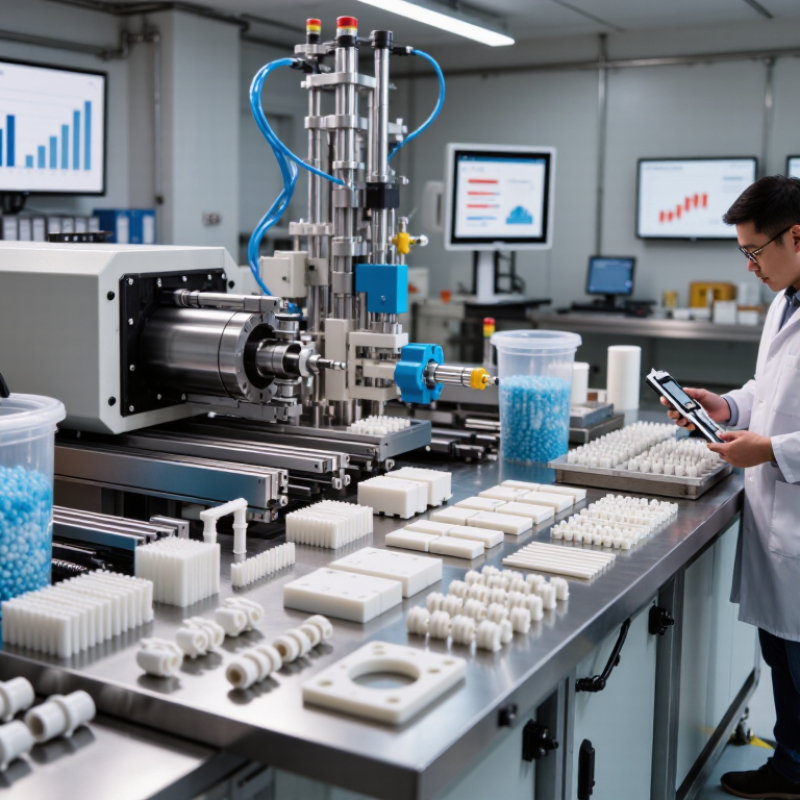
Choosing a precision plastics manufacturer begins with a usable specification, not a machine list. ISO 20457:2018 provides tolerance and acceptance guidance for moulded plastic parts; it does not select the resin or guarantee fit. Name the resin grade, color, fillers, and any recycled content. Small changes matter. PlasticsEurope’s Plastics—The Fast Facts 2024 reports 413.8 million tonnes of global plastics production in 2023. That scale does not mean materials behave uniformly.
Then define geometry and critical dimensions. A 20 mm snap-fit, thin rib, or thick boss can cool differently and shift after ejection. Mark datums, mating surfaces, and dimensions that affect assembly; avoid tight tolerances on every feature. Apply ISO 20457’s tolerance framework where appropriate, then call out function-critical limits explicitly. Ask how shrinkage, draft, gate location, and conditioning affect the drawing. Not every risk is obvious on CAD.
Request a capability review using the actual resin and representative geometry, followed by first-article measurement. Ask which features are measured, with what equipment, and under what temperature or moisture conditions. A tolerance is only useful when inspection conditions are repeatable. Early drawings are often incomplete; review them rather than guess. Tooling can lock in a compromise that looked harmless on screen.
How to Choose a Precision Plastics Manufacturer? — Define Resin, Geometry, and Tolerances with ISO 20457:2018
| Decision Area | Information to Define | Practical Example | What to Confirm with the Manufacturer | ISO 20457:2018 Consideration |
|---|---|---|---|---|
| Resin and grade | Specify the polymer family, exact grade where known, colour, additives, and any regulatory or environmental requirements. | Unfilled polycarbonate for impact-resistant, transparent components; glass-fibre-reinforced polyamide for applications requiring greater stiffness. | Ask for the grade’s technical data sheet, material traceability, drying requirements, and confirmation that the selected grade suits the part’s service environment. | Material choice and processing affect dimensional behaviour. Agree on the actual material and relevant acceptance requirements before setting tolerances. |
| Service conditions | Describe operating temperature, moisture exposure, chemicals, UV exposure, mechanical loads, and expected service life. | A polyamide component exposed to moisture may change dimensions as it absorbs water; a component near a heat source may require evaluation at its operating temperature. | Confirm whether dimensions must be assessed as moulded, conditioned, or after exposure to defined service conditions. | Acceptance conditions should reflect the agreed state and inspection conditions of the part, rather than relying on an unspecified measurement state. |
| Part geometry | Provide a fully dimensioned drawing or 3D model, including wall sections, ribs, bosses, draft, radii, openings, and datum features. | Use consistent nominal wall sections where practical, and identify critical mounting faces and locating features on the drawing. | Request a design-for-manufacturing review covering mould filling, cooling, ejection, likely warpage, and access for inspection. | Geometry and moulding conditions influence attainable dimensional accuracy. Identify critical features and agree how they will be evaluated. |
| Functional tolerances | Set tolerances from assembly fit, sealing, movement, alignment, or other functional needs—not from a preference for the smallest possible number. | Specify a tighter tolerance on a locating bore if assembly depends on it, while allowing a more suitable tolerance on a non-functional external surface. | Ask the manufacturer to review each critical dimension for capability and to identify any tolerance that may require tooling or process changes. | Use ISO 20457:2018 as the reference framework for moulded-part tolerances and acceptance conditions. State the selected requirements on the drawing or in the purchase specification. |
| Dimensions and datums | Define measurement datums, measurement points, and whether dimensions apply to the complete part or a specified feature. | Reference a mounting face as datum A and define hole position relative to the agreed datum structure. | Agree on a measurement method—such as a calibrated instrument or coordinate measuring machine—and ensure the part can be fixtured consistently. | Clear drawing requirements and agreed inspection conditions help avoid differing interpretations of tolerance and acceptance. |
| Tooling and process | Define the intended moulding process, number of cavities where relevant, and ownership or maintenance expectations for the mould. | For a multi-cavity tool, identify whether cavity-to-cavity variation must be assessed separately during qualification. | Ask how the supplier will control process changes, cavity identification, tool maintenance, and production start-up approvals. | Tolerances should be agreed with the actual part, material, tooling, and production conditions in view; a standard reference does not guarantee a specific capability for every feature. |
| Inspection and approval | Define the sampling plan, first-article requirements, inspection report format, and treatment of nonconforming parts. | Request dimensional results for designated critical features during initial approval and after agreed changes to material or tooling. | Confirm measurement equipment, calibration status, reporting units, and the procedure for resolving measurement disagreements. | Document the applicable edition, tolerance requirements, acceptance conditions, and any agreed exceptions in the technical documentation. |
Note: ISO 20457:2018 provides a framework for tolerances and acceptance conditions for plastics moulded parts. It does not replace part-specific drawings, functional requirements, or agreement on material, measurement conditions, and inspection methods.
Related Posts
-
Why is Plastic Fabrication Important for Modern Industries?
-
2026 Top Trends in Plastic Fabrication Innovations and Applications?
-
What are the Best Plastic Molding Machines of 2026?
-
2026 How to Find the Best Injection Molding in Las Vegas?
-
Why Choose Injection Molding Services in Las Vegas?
-
Top Plastic Parts Innovations in Modern Manufacturing?